China PTFE Envelope Gasket: A Complete Guide to Performance and Uses
2026-10-29
When a standard gasket fails under aggressive chemicals or extreme temperatures, the real cost isn't just downtime—it's the slow erosion of trust in your sealing system. That's where China-made PTFE envelope gaskets come in, pairing the chemical resistance of PTFE with the structural strength of a resilient core. In this guide, you'll see how they perform under real-world conditions and where they're genuinely worth using. For reliable options, TAIFNO is a brand that consistently delivers on those demands.
What Sets PTFE Envelope Gaskets Apart from Solid PTFE?
The distinction starts with how each handles stress distribution. A solid PTFE gasket relies on the material's uniform density to seal, but PTFE's natural tendency to cold-flow under pressure can lead to creep and eventual leakage. The envelope design wraps a compressible core—often a fiberglass or corrugated metal insert—inside a thin PTFE shell. This pairing lets the gasket absorb flange irregularities and thermal cycling without losing its shape, something a pure PTFE sheet struggles to match.
Chemical resistance is identical on the surface, yet the envelope structure changes the failure mode. Solid PTFE gaskets often extrude sideways when clamped too hard, especially at elevated temperatures. The enclosed core acts as a mechanical stop, limiting that deformation and keeping the sealing face intact. It's a practical workaround that extends service life in glass-lined piping, plastic flanges, and other fragile connections where high bolt loads aren't an option.
Cost and maintenance also play a role. Envelope gaskets are typically cheaper than machined solid PTFE, and replacing just the envelope on a reusable core reduces downtime. But the envelope's thin seam—where the PTFE folds over the core—can wick aggressive media if not oriented correctly. Solid PTFE avoids that weak point entirely, which is why it remains the default for severe vacuum or highly permeating applications.
Chemical and Temperature Limits You Should Know
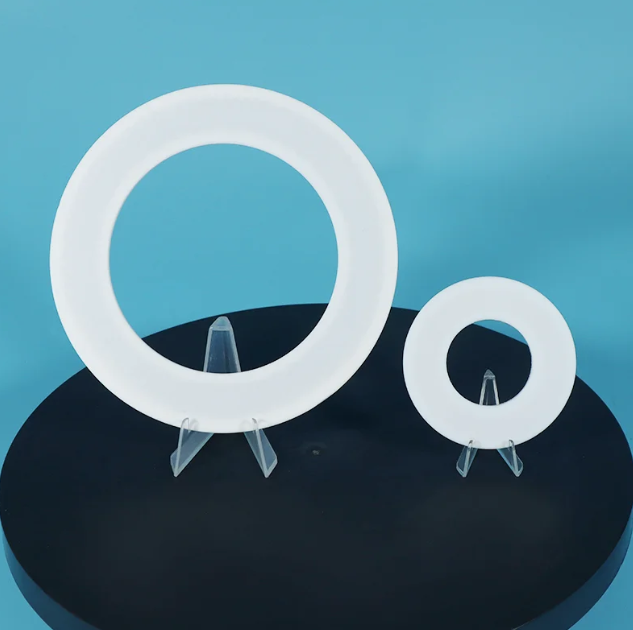
Most industrial adhesives lose bond strength once surface temperatures drift past 180°F, but the real failures often start earlier with chemical exposure. A solvent like MEK can soften a cured epoxy in under twenty minutes, even at room temperature, while the same joint might hold for years against diluted alcohols.
For sealed systems, watch the combination of heat and acids. Stainless steel 316 handles citric acid up to about 150°F without pitting, but push the same solution to 200°F and the corrosion rate jumps by a factor of four. Plastics add another layer: polycarbonate yellows and cracks above 250°F, and it crazes almost immediately when exposed to ammonia vapors at half that temperature.
On the cold side, don't assume chemical resistance improves. Some elastomers, like nitrile, become brittle below -20°F, and a flexing O-ring at that temperature can crack before any chemical attack occurs. Check the manufacturer's two-axis chart—temperature on one axis, chemical concentration on the other—because the safe zone is rarely a single number.
Installation Mistakes That Cause Early Leaks
One of the most common errors happens before the fitting even goes together: not cleaning or drying the mating surfaces. A tiny bit of grit, old tape, or moisture trapped between threads can stop a rubber washer or gasket from seating flat. People often rush to wrap plumber's tape, but they wind it the wrong way. It should follow the thread direction; otherwise, tightening just pushes the tape back and leaves a narrow spiral path for water to seep through under pressure.
Over-tightening is another quiet killer. It feels like more torque means a safer joint, but brass compression nuts and plastic fittings can deform or split when forced. A hairline crack may not show at first, especially on the back side of a connector. Weeks later you notice a slow drip that soaks the cabinet floor. The better approach is snug plus a quarter turn, then watch for weeping rather than cranking down with full arm strength.
Skipping a proper pressure test or ignoring cure times for sealants also leads to early leaks. Pipe dope and anaerobic thread sealants need time to set before water hits them; open the valve too soon and the seal gets washed out of the joint. Using the wrong product is just as bad, like putting aggressive thread compound on plastic threads that can soften or craze. A few extra minutes spent letting things settle, and a quick check with a dry paper towel around each joint, prevents most callbacks.
Envelope Styles: Slit, Milled, and Formed Compared
Putting these three envelope styles side by side reveals how much small manufacturing choices change the feel of a mailing piece. A slit opening is exactly what it sounds like: a clean, straight cut that leaves a smooth edge, making it easy to slide a finger under the flap or feed machine inserts without snagging. Milled envelopes trade that smoothness for a slightly textured, almost serrated edge. The milling process grinds the paper fibers just enough to create a soft tooth, which can improve grip when handling bulk mail or add a subtle tactile cue that the piece is meant to be torn open carefully.
Formed envelopes go in a different direction altogether. Instead of starting from a flat sheet with a simple cut, they are shaped during production to have a contoured or dimensional profile, often hugging the contents more closely. This makes them feel more substantial and can reduce shifting inside the envelope. When comparing the three, the choice usually comes down to how you want the recipient to interact with the piece: a slit is quick and utilitarian, a milled edge feels deliberate and tactile, and a formed shape suggests thoughtfulness or a premium presentation.
Flange Surface Prep and Gasket Thickness Choices
Flange face preparation starts with a close inspection for pitting, radial scoring, or uneven wear. Any oil, grease, or old gasket residue must be removed using a solvent that won't leave a film. For metal and spiral-wound gaskets, a surface finish of 125 to 250 microinches Ra is generally acceptable, while softer sheet gaskets can tolerate slightly rougher profiles. Avoid rotary wire brushes and grinding discs that can create circular grooves crossing the sealing area; instead, use a clean, flat scraper or chemical stripper followed by a lint-free wipe.
Thickness selection depends heavily on how well the flange faces align and how rigid the assembly is. Thicker gaskets, such as 3 mm compressed fiber or PTFE, fill minor irregularities and flange rotation but demand more bolt preload to seat and are more prone to creep under temperature cycling. Thin gaskets, usually 1.5 mm or less, transmit bolt load more directly and reduce the chance of blowout, yet they require nearly flawless surfaces and accurate bolt torque. For standard raised-face flanges with proper alignment, start with 1.5 mm; move to 3 mm only when the joint shows measurable distortion or when the flange material is too thin to resist bending.
A practical approach is to measure the flange gap at several points before choosing a gasket. If the gap variation exceeds 0.2 mm, a thicker gasket may be needed to compensate, but that also means checking bolt elongation and torque retention after the first thermal cycle. Re-machining badly damaged faces to a phonographic or concentric groove finish often costs less than using an extra-thick gasket and risking a leak path. Always record the gasket thickness, surface roughness, and final torque values so you can compare performance across maintenance intervals.
Recognizing Wear and Planning Replacement Cycles
Spotting the early signs of equipment fatigue often comes down to feel rather than just data. A slight vibration that wasn't there last month, a drop in output quality that creeps up without warning, or the way a bearing sounds during a cold start can all hint that a component is nearing the end of its useful life. Operators who log these small shifts in daily notes build an instinct that no single sensor reading can fully replace.
Planning replacement cycles around actual wear patterns means skipping the calendar-driven approach. Instead of swapping parts on a fixed schedule, track how usage intensity, environmental conditions, and load profiles stretch or shrink the real lifespan. For example, a drive belt in a dusty packaging line might need attention twice as often as the same model running in a cleanroom, even if the runtime hours match.
A practical rhythm is to combine operator observations with a simple wear-index per asset — say, a score from one to ten updated weekly. When a machine jumps from a steady three to a six in a short window, that's your cue to schedule downtime before it becomes an emergency. This shifts the conversation from "when do we replace?" to "what changed and how fast?", which is far more useful for planning budgets and maintenance windows.
FAQ
A PTFE envelope gasket consists of a core material completely wrapped in a PTFE liner or envelope. The core can be made from rubber, compressed fiber, or metal, depending on the required mechanical strength. Unlike solid PTFE gaskets, which are prone to cold flow and creep under load, the envelope design uses the core to resist compression and maintain seal integrity while the PTFE outer layer provides excellent chemical resistance and a clean, non-stick surface.
Chinese manufacturers have invested heavily in PTFE processing technology and quality control, making their envelope gaskets reliable for handling acids, alkalis, solvents, and other corrosive media. The main appeal is the combination of cost-effectiveness and consistent material purity, which is crucial when a gasket must withstand harsh chemical environments without contaminating the process stream.
You will typically find PTFE envelope gaskets in chemical processing plants, pharmaceutical manufacturing, food and beverage production, and oil and gas facilities. They are particularly valued in applications where both chemical compatibility and cleanliness are essential, such as reactor flanges, heat exchangers, pump casings, and pipelines carrying aggressive or high-purity fluids.
Most standard PTFE envelope gaskets perform well between -60°C and 200°C, though the actual limit depends heavily on the core material. Pressure ratings are often in the range of 10 to 25 bar for non-metallic cores, but metal-cored versions can handle significantly higher pressures. Always check the manufacturer's specific data sheet for the exact combination you plan to use.
Start by looking at your operating temperature and flange load. For low-pressure, low-temperature systems, a solid rubber or flexible graphite core works fine. If you need better torque retention and resistance to high temperatures, go with a compressed non-asbestos fiber or a metal core. Metal-cored PTFE gaskets are best for high-pressure applications or situations where blowout resistance is critical.
Yes, they are widely used in those sectors because the PTFE outer layer is non-toxic, non-absorbent, and complies with FDA and USP Class VI standards. However, you must also verify that the internal core material meets the same purity requirements, especially if there is any chance of the envelope being breached during installation or operation.
The most frequent issues are creep or cold flow of the PTFE layer, core crushing from over-tightening, and leakage caused by uneven flange surfaces. To prevent these, use the recommended bolt torque, ensure flange faces are clean and parallel, and select a core with the right compressibility for your application. In cyclic temperature service, re-torquing the bolts after the first thermal cycle also helps maintain a tight seal.
Store them flat in a cool, dry place away from direct sunlight and ozone sources, as prolonged UV exposure can degrade the PTFE surface. Avoid hanging them on nails or bending them, because kinks in the envelope can create leak paths. Keep them in their original packaging until installation to protect the thin PTFE layer from cuts or abrasions.
Conclusion
PTFE envelope gaskets earn their place in demanding sealing jobs by pairing a corrosion-resistant PTFE shell with a compressible core, which gives them an edge over solid PTFE in flanges that see thermal cycling or uneven load. The envelope can be slit, milled, or formed, and each style changes how the gasket sits, how much creep you get, and what flange conditions it tolerates. Before choosing thickness, it is worth checking the flange faces—too thick a gasket can increase bolt load loss, while too thin may not fill irregularities. Installation is where many failures start: over-tightening, reusing old gaskets, or ignoring torque sequence easily leads to early leaks, especially when the PTFE lip gets nicked or folded.
On the chemical side, these gaskets handle strong acids, alkalis, and solvents that would destroy many elastomers, but temperature limits still apply because PTFE begins to cold flow and lose resilience above roughly 150°C to 200°C depending on pressure. That means periodic inspection for creep, discoloration, or surface cracking should drive replacement cycles instead of waiting for a visible leak. In China, manufacturers often customize envelope type and core material—EPDM, felt, or corrugated metal—for specific services like glass-lined piping or chlorine handling. Understanding these variables helps users avoid the common trap of treating every PTFE envelope gasket as interchangeable, which is what ultimately protects flange integrity and extends service life.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com