Chocolate Enrober Factory Essentials for Perfectly Coated Confections
2026-11-21
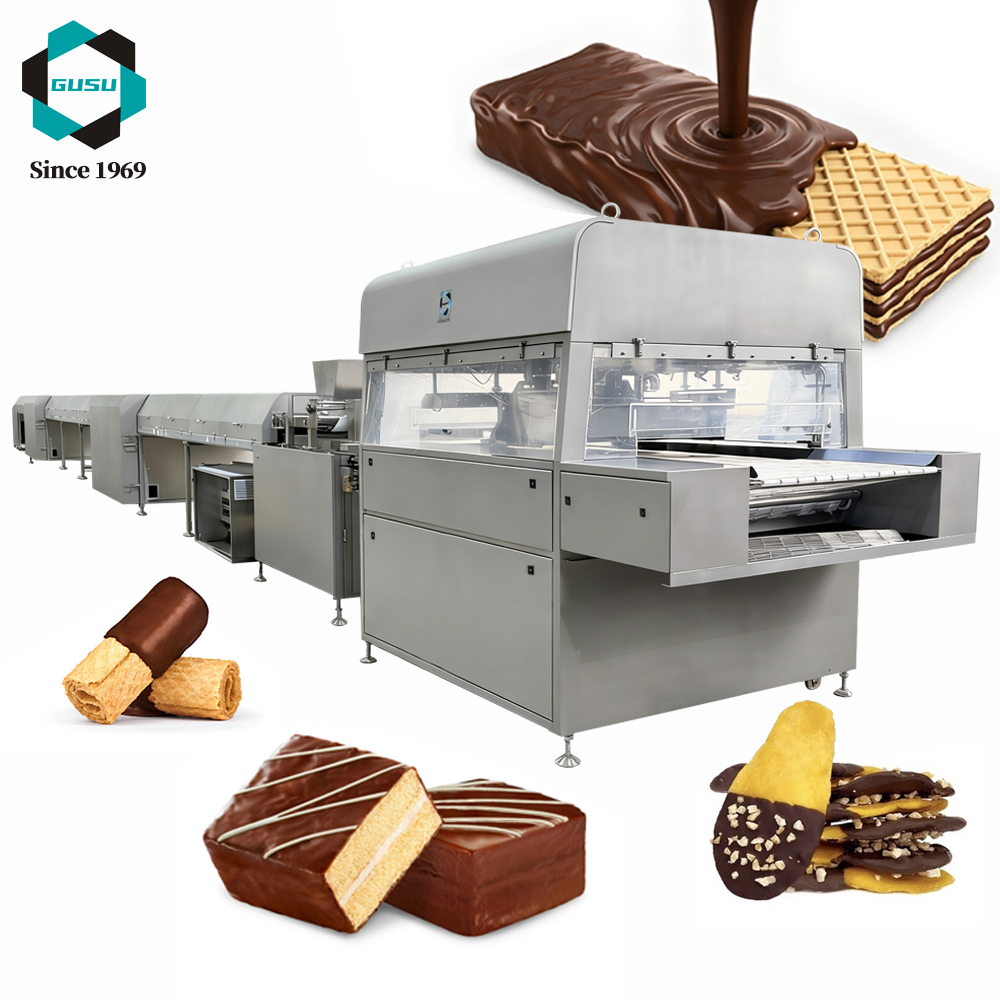
Most coating problems don’t start at the enrober—they start with the details around it. From viscosity control and tempering stability to airflow and belt speed, the gap between a dull finish and a flawless shell often comes down to factory essentials most teams overlook. Here’s what GUSU has learned about building a line that delivers repeatable, perfectly coated confections.
Dialing In Temper Before the First Piece Hits the Belt
Most tempering problems are locked in before the enrober ever starts. I keep a small bowl of unmelted seed chocolate next to the tempering kettle and check the working temperature with two thermometers, not one. Dark chocolate usually wants to come down to about 88-90°F before it goes to the wheel; milk and white sit a couple degrees lower. If the batch has been sitting, I stir the bottom hard and recheck. A clean spatula dipped in the chocolate should set with a faint snap within two minutes against the side of the bowl, not tacky, not dull gray.
The real test is what the chocolate does on a strip of parchment, not what the thermostat says. I pour a thin ribbon, let it rest, and watch the surface. A properly tempered batch turns matte at the edges first, then firms evenly without blooming. If it stays wet or oily in the center, I seed in small amounts and wait. Rushing that wait only shifts the problem downstream, where it becomes a belt full of streaked pieces no one wants to scrape off.
Once the temper holds for two strip tests back to back, I let the first piece hit the belt and then pull it immediately. That first piece tells more than a dozen later ones. I break it, look at the snap, and rub a thumb across the surface. Only then do I turn the line up to speed.
Airflow Patterns That Preserve Shine and Snap
Most blow dryers blast air straight down the hair shaft, which can flatten the cuticle unevenly and kill the natural bounce. A better approach is to angle the nozzle so air flows along the cuticle's grain, from root to tip, but with a slight lateral wobble. This keeps the outer layer smooth without pressing it flat, so light still reflects off the surface while the strand retains its built-in spring. The trick is not constant heat or maximum speed, but a gentle, shifting airflow that lets each section cool in its lifted position before you move on.
For curls and waves, the worst enemies are blast-dryer chaos and over-brushing. Instead, use a diffuser with shallow, cupped airflow that hovers around the curl cluster rather than pushing through it. The goal is to dry the outside of each spiral while the inner structure stays slightly damp longer, which helps the pattern lock without turning crunchy. After the hair is eighty percent dry, switch to a cool, low-flow setting and lift sections with your fingers, letting the air trace the curve instead of blowing it apart. That final pass is what brings out shine without sacrificing the snap of a well-formed curl.
A less obvious pattern is the two-zone method. Start at the roots with a narrow nozzle and medium airflow, moving in short diagonal strokes to build lift without roughing the scalp area. Once the root zone feels warm but not hot, switch to a wider, softer flow for the mid-lengths and ends, keeping the dryer at least six inches away. This sequence mimics how hair dries naturally after a swim or a light rain, but with enough control to polish the outer layer. The result is hair that swings when you turn your head and still catches the light in a single, clean line.
Matching Belt Speed to Viscosity for Clean Edges
Getting clean edges starts with understanding how the fluid responds to movement. A low-viscosity adhesive or coating tends to spread quickly, so running the belt too slowly gives it time to bleed past the intended boundary. On the other hand, a thick, paste-like material may hold its shape at first, then stretch and leave tails or rough edges when the belt pulls away too fast. The goal is to keep the material under enough tension to separate crisply, but not so much that it smears before it sets.
Small speed adjustments are usually more effective than large ones. If the edges start to look feathered or wet, increase the belt speed in short increments or reduce the application temperature slightly so the viscosity firms up. If the edges appear torn, uneven, or lifted, slowing the belt gives the material a moment to relax and settle before it leaves the dispensing or coating zone. Watching the edge for two or three full cycles after each change will tell you more than any preset chart.
It also helps to keep a simple log for each material batch. Note the belt speed, temperature, and edge result for a given viscosity range, then use that as a starting point for the next run. Over time, this builds a practical feel for how the line should sound and look, and edge issues become quicker to trace before they turn into waste.
Nozzle Height and Curtain Stability Under Real Loads
Real operating conditions rarely mirror the clean, steady flows assumed during initial calibration. When a curtain of air or liquid is pushed by sudden cross-drafts, uneven floor loads, or shifting thermal gradients, the nozzle height stops being a simple setpoint and becomes a live variable. A unit mounted too high loses its hold on the target surface, letting the curtain drift and fold under moderate pressure fluctuations. Mounted too low, it creates an over-compressed zone that bounces back, producing visible flapping at the edges. The practical window for stable operation narrows sharply once the load deviates from a flat, uniform profile.
Field adjustments tend to chase symptoms rather than causes. One common pattern is raising the nozzle in response to edge leakage, only to trigger mid-span sag when a passing forklift shifts the local airflow. Another is lowering it aggressively to fight billowing, which then scrapes uneven pallets and wears the lip seals unevenly. What stabilizes the curtain in one corner of a busy dock often destabilizes it twenty meters away. Operators learn to read the ripple pattern: short, rapid flutter usually points to excess velocity at the gap, while slow, broad waves suggest the discharge is losing attachment and reattaching in cycles tied to building pressure.
The fix usually involves accepting that no single height works for every load. Instead, the nozzle position should respond to the highest expected disturbance at the point where the curtain meets the floor or sill. Accelerometer traces or high-speed video from a few seconds of actual operation tell more than a week of static testing. On retrofit projects, adding a slight downstream deflection or a removable lower guide can extend the stable range without chasing micron-level height changes. When the curtain holds its line under a truck passing three meters away or a dock door slamming open, the height setting has earned its place.
Routine Clean-In-Place Steps That Prevent Flavor Drift
Flavor drift rarely announces itself with a visible mess. Most of the time it starts as a thin protein-oil film or a haze of beerstone that changes how the next batch picks up bitterness, sweetness, or metallic edges. A routine clean-in-place cycle should therefore begin with a pre-rinse that actually removes loose soil before heat or caustic can bake it onto the surface. Run the water until it clears, not until a fixed timer expires, and pay attention to return-line clarity at the drain. If the first rinse looks milky or carries hop specks, the rest of the cycle is already fighting leftover residue.
The middle of the cycle is where order and concentration matter more than total chemical contact time. Caustic should handle organic films, while an acid step handles mineral scale such as beerstone; swapping these or letting either solution fall below its effective temperature or concentration leaves a layer that can hold onto flavor compounds. Check the return line during recirculation for temperature and conductivity rather than assuming the tank is clean because the pump ran. A few degrees too cool or a slightly depleted caustic bath can leave a nearly invisible film behind, and that film becomes the baseline flavor for the next batch.
Finish with a rinse that proves the chemicals are gone, not just that the water looks clear. Run until the pH stabilizes near neutral and there is no slick feel on a clean glove wiped across a shadow zone like a gasket, dead leg, or spray ball shadow. These low-flow areas are where flavor drift hides because they receive less mechanical action during the cycle. Swabbing or smelling the final rinse water is not excessive; it is a simple check that the tank has been returned to a neutral starting point rather than carrying a trace of caustic, sanitizer, or stale product into the next brew.
Profile Settings by Couverture Type and Inclusion Density
Dark couverture with 70% cocoa solids behaves nothing like a milk chocolate at 38%. The fat crystal structure shifts, viscosity climbs, and your tempering curve needs to bend accordingly—what works for one will streak or bloom on the other. Profile settings that tie temperature ramps and agitation speed directly to couverture type prevent those grainy edges and dull patches that show up hours after enrobing.
Then there is the inclusion load. A sparse dusting of crushed hazelnuts barely changes flow, but a dense mix of biscuit crumbs and freeze-dried raspberry pieces turns the same couverture into a slow, lumpy slurry. Raising the pump pressure a notch and widening the curtain gap usually solves it, though you will also need to adjust the vibration frequency so the inclusions settle without trapping air. Getting that balance right means fewer reworks and a cleaner break line on the finished piece.
FAQ
Going too thick to make sure coverage is complete. A heavy curtain floods the detail work on molded pieces and buries sharp edges. Start thinner than feels safe, then open the gate just until the trailing side stops showing bare spots. That usually leaves a cleaner foot and fewer blower passes.
The chocolate in the trough may be tempered, but vibration and return scrap can knock it out slightly. Dull streaks often point to a return chocolate stream that is too hot or too cold hitting the main bath, or a curtain that is uneven side to side. Check the return temperature and the distribution baffle before blaming the tempering machine.
Enough to keep the edge of the curtain from pulling inward as it falls, usually about 15 to 25 mm each side, but no more than needed. Too wide an overhang just increases scrap and provides another spot for chocolate to hang and drip onto the next row unpredictably.
Look at the blower angle before changing speed. A blower aimed too straight down presses the product into its own puddle and can actually increase the foot. Tilt the airflow slightly back against the direction of travel so it sweeps the excess rearward without driving coating under the piece.
Install a small heated baffle or keep the enrober hood warm and draft-free, and feed tempered chocolate on a level-controlled loop rather than in large batch additions. Large top-ups swing the working temperature. Steady level and gentle agitation keep viscosity from creeping up, so the curtain behaves the same hour after hour.
Yes for flat-bottomed centers. It gives a controlled base layer so the main curtain only has to seal the sides and top. Without it, the belt itself carries chocolate under the centers, but that layer depends on belt speed, scraping, and trough depth, which are harder to keep constant.
Leaving the return tray or blower nozzles coated overnight and just reheating them the next morning. Partially melted residue breaks free into the bath as small lumps, which then show up as bumps or comet tails on coated pieces. Scrape and wipe those areas at the end of every run while the chocolate is still soft.
Because the piece spends too long in the blower zone or the blower pushes excess chocolate off the top but not off the trailing edge. Shorten the tail by trimming the curtain slightly at the gate or increasing the belt speed a touch, then use a light air kiss instead of a hard blow.
Conclusion
Temper control has to be settled long before the first centre touches the belt, because even a small drift in cocoa butter crystallization will show up later as dull patches or weak snap. Rather than relying on a single reading, experienced operators watch the viscosity at the depositor and check the surface gloss during early trials. The air handling around the curtain is just as critical. Uneven plenum pressure can cool one edge faster than the other, leaving the coating lopsided and streaky. Belt speed then needs to match the way the couverture actually flows, not the nominal pump setting. High-viscosity dark chocolate tends to drag and tail if the belt runs too fast, while thinner milk chocolate can flood the sides when it runs too slow. Nozzle height is adjusted under real load because a stable falling curtain at idle often breaks apart once product mass and line vibration enter the picture.
Clean-in-place is treated as part of flavour management, not just sanitation. Residual cocoa butter trapped around baffles or return chutes oxidizes and carries stale notes into fresh batches, so rinse cycles and drain intervals are scheduled around what is actually being run. That matters most when switching between high-fat hazelnut inclusions and delicate fruit centres, where flavour drift becomes obvious. The final layer of consistency comes from stored profile settings that account for couverture type and inclusion density. White chocolate with crushed freeze-dried raspberry behaves nothing like a fluid dark blend with finely milled nuts, so each profile ties temper targets, air velocity, belt speed and nozzle gap to the specific material. Operators who treat those settings as starting points rather than fixed recipes tend to get cleaner edges and better shine across shifts.
Contact Us
Contact Person: Zhang Wei
Email: [email protected]
Tel/WhatsApp: 8618662577837
Website: https://www.chocomachinery.com