Recycled Material Filler Pad Distributor Options That Reduce Waste and Cost
2026-11-22
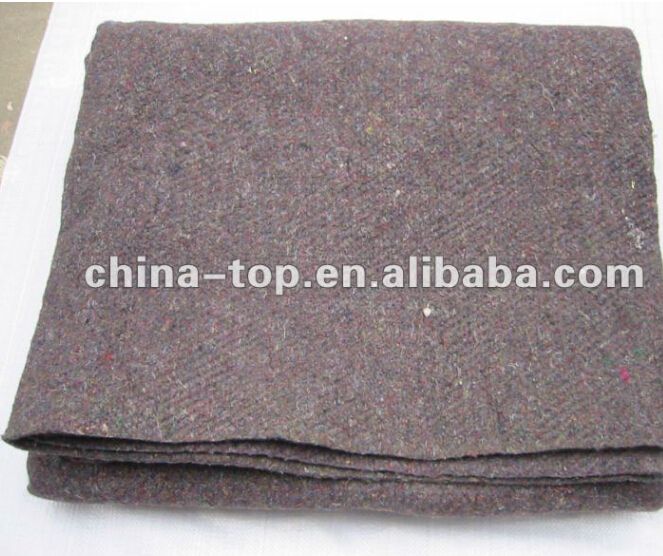
Filler pads rarely get much attention—until the invoices and waste reports come in. Recycled material filler pads offer a smarter middle ground for distributors: less packaging waste, lower per-shipment cost, and dependable protection. At Top Packaging, we see more teams making the switch, but not all options are equal. Here's what to look for before you choose.
Distributors That Actually Verify Recycled Content
Plenty of distributors put a green label on a spec sheet and call it a day. The ones worth working with are different: they can show you batch-level documentation, supplier audit results, and a chain of custody that holds up when you start asking questions. Recycled content claims fall apart quickly without that paper trail, and they know it.
What separates a genuine verification process from a marketing line is how the distributor handles variability. Post-consumer and post-industrial feedstock changes by season, region, and collection stream. A distributor that actually verifies recycled content will test incoming lots, flag out-of-spec material, and adjust formulations instead of quietly swapping in virgin resin to hit a performance target.
It also shows up in their relationships. You will notice they can name the reclaimers, describe how the material is sorted and washed, and explain what happens when a supplier misses a target. If that information is hard to get, the recycled content claim is probably not as solid as the data sheet suggests.
Regional Sourcing Moves That Trim Freight and Fees
A consumer goods importer near Columbus pulled injection-molded parts from two Asian suppliers into a network of molders in Nuevo León and El Paso. The piece price edged up about four percent, but freight landed lower almost immediately. Port handling and chassis fees that had been running roughly $180 per pallet went away, and transit time dropped from five weeks to six days. Those two line items alone changed the math.
The bigger shift came in how loads are built. Instead of dragging 40-foot containers from Long Beach and Newark to a Kansas City DC, the team now runs scheduled 53-foot dry van routes across three nearby states. Fewer handoffs mean fewer accessorial charges for detention, appointment misses, and reconsignment. Invoices are easier to audit because there are simply fewer of them.
Sourcing closer to demand also tightened inventory planning. Lead time variability narrowed enough that the buying team cut safety stock from about seven weeks to two and stopped reserving airfreight budget for routine replenishment. The savings show up outside the freight rate itself, in lower carrying costs, less expediting, and fewer exceptions requiring manual approval.
Bulk Order Setups That Lower Cost Without Extra Inventory
Bulk order pricing usually comes with a hidden assumption: you have to buy more than you need. But a smarter setup flips that idea. Instead of tying up cash in extra stock, you negotiate tiered rates that unlock at a lower breakpoint, or you work with suppliers who hold the surplus for you until actual demand shows up. The result is a unit cost that drops sharply without your warehouse becoming a storage locker for slow movers.
One practical route is to split a single large purchase order into multiple scheduled releases. You get the volume discount for the total quantity, but payment and delivery happen only when each batch is called off. Another angle is to consolidate orders across a few related products that share core materials, so the factory sees one big production run while you avoid overcommitting to any single SKU. In both cases, the key is treating the order agreement, not the physical inventory, as the cost lever.
The suppliers that cooperate with this approach are usually the ones you have built a steady, reliable rhythm with. They value your recurring business more than a one-time spike in volume. Ask them what their actual setup or changeover costs are; once you understand that, you can propose a structure that lets them keep machines running efficiently while your cash stays free. Lower cost, no extra shelf weight.
Custom Sizing Programs That Reduce Offcut Waste
Material waste often starts well before a saw touches the sheet. Standard panel sizes push workshops into buying more board area than a job actually calls for, leaving narrow strips and odd rectangles that tend to sit unused. Custom sizing programs break that pattern by matching orders to the nearest workable dimensions from the beginning. Instead of trimming a full sheet down by a large margin and hoping the leftover finds a future purpose, the supplier cuts closer to the required sizes before delivery. That simple shift removes a large share of offcut waste at the source.
The practical difference also shows up in storage and workflow. When remnants shrink to a few clearly usable pieces rather than an overflowing pile, racks stay easier to organize and the leftovers become easier to reuse. Some shops build small labeled libraries of these offcuts, sorted by thickness and finish, so a future drawer component or shop jig can pull from existing material instead of breaking into a new sheet. Leftover handling starts to feel less like a periodic cleanup task and more like a quiet part of daily material flow.
Mixed panel jobs bring another advantage. A cutting list with many different dimensions can be checked against sheet yield before any physical cutting happens. Custom sizing allows the supplier to group pieces intelligently across several boards, sometimes recovering enough usable area to remove an entire extra sheet from the order. Across repeated projects, that efficiency compounds into lower material spend and far less waste reaching the bin.
Take Back and Reclaim Options Many Suppliers Keep Quiet
Most buyers never hear about the quieter return channels until something sits too long on a shelf or a seasonal line stops moving. Suppliers may mention restocking fees, but they are far less likely to volunteer that they will accept unopened cartons after sixty days, apply credit toward a future order, or take back slow sizes in exchange for faster inventory. These options exist to keep the relationship alive, not because anyone wants to advertise them. Ask in plain terms before signing: what happens at day ninety, who pays return freight, and whether credit is applied at invoice level or held as a separate balance.
Reclaiming value often depends on how the request is framed. A supplier is more willing to bend when you show a plan for the returned stock, such as clearing warehouse space for a new collection or consolidating open-box units into one selling channel. Instead of asking for a refund, ask for a swap, a credit note, or a partial allowance that lets you discount the product locally without destroying the supplier’s pricing structure elsewhere. The goal is not to force a concession, but to surface the unofficial path the supplier already has for accounts that ask the right way.
Lifecycle Cost Checks When Virgin Material Is No Longer Cheapest
When virgin material stops being the cheapest option on paper, a one-line price comparison becomes the weakest way to choose a feedstock. The lower sticker price can come with narrower processing conditions, more rejects, or longer drying times, and those operational burdens stay invisible until a full production run is measured. At that point the material with the lowest invoice rarely matches the material with the lowest cost per usable part.
A practical lifecycle check starts with a fixed batch or shift, not a per-ton quote. Track energy use, regrind losses, labor spent on inspection and rework, waste disposal, and any time lost to trial runs or equipment cleanouts. Recycled and blended grades often perform better under this wider view because consistency and process stability matter more than a small difference in raw material price.
The goal is not to favor one type of material. It is to make sure a purchasing decision is not driven by an incomplete number. Once these hidden costs are included, a material that looked cheaper by weight can easily become the more expensive choice across a month of production.
FAQ
Look for documented material sources, consistent density and thickness across batches, and the ability to match your existing equipment without forcing a line change. A dependable supplier also offers small trial runs before you commit to full volumes.
Savings usually come from three places: lower raw material pricing, reduced waste disposal charges, and sometimes lighter pad weights that trim freight costs. The exact figure varies by volume, but double-digit percentage savings on filler material are common once the switch is fully implemented.
Modern recycled pads can perform very close to virgin equivalents when the distributor controls input quality well. Ask for compression test data and request samples from multiple production runs rather than relying on a single batch.
Yes, many distributors offer custom cutting, scoring, and lamination. The key is to share your line specs and damage history early so the pads are designed around your actual handling conditions instead of a generic template.
Common inputs include post-industrial corrugate, mixed paper fiber, reclaimed foam, and reprocessed plastic film. Some pads blend materials to balance cushioning and stiffness, so it is worth asking for the exact recycled content percentage.
Request third-party certifications, chain-of-custody documentation, or a material traceability report. A credible distributor will also explain how returned or off-spec pads are handled, including whether they can be fed back into the same recycling stream.
Watch for tooling or setup fees, minimum order quantities, freight distance from the distributor’s warehouse, and the cost of trialing new pad dimensions on your packing lines. These items can offset the per-unit savings if they are not reviewed up front.
Conclusion
Sourcing filler pads made from recycled material only pays off when the distributor can show what is actually in the sheet. A handful of suppliers now attach batch-level documentation or third-party test data, which makes it easier to avoid paying a green premium for material that is only lightly reclaimed. Pairing that verification with regional distribution cuts a surprising amount of freight and handling cost, especially for bulky low-density pads. Where possible, consolidating orders around predictable sizes rather than holding extra safety stock tends to lower unit pricing without forcing a warehouse full of slow-moving inventory.
Custom sizing programs are another overlooked lever. When pads are cut closer to finished dimensions, less material ends up in the scrap bin, and that offcut reduction often outweighs a slightly higher per-sheet price. Some distributors also run quiet take-back or reclaim routes for used pads and edge trim, which can trim disposal fees and feed material back into lower-grade products. Finally, run the numbers on total lifecycle cost instead of assuming virgin sheet is cheaper; freight, scrap, disposal, and reorder frequency sometimes flip the comparison in favor of recycled stock.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 86-577-64286522
Website: https://www.topmovingpad.com/